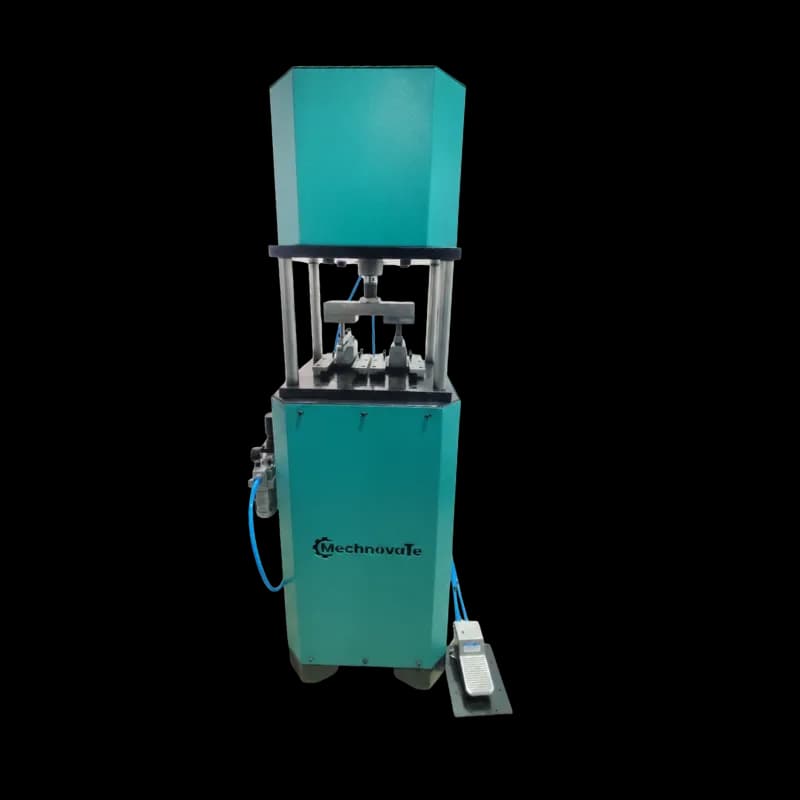
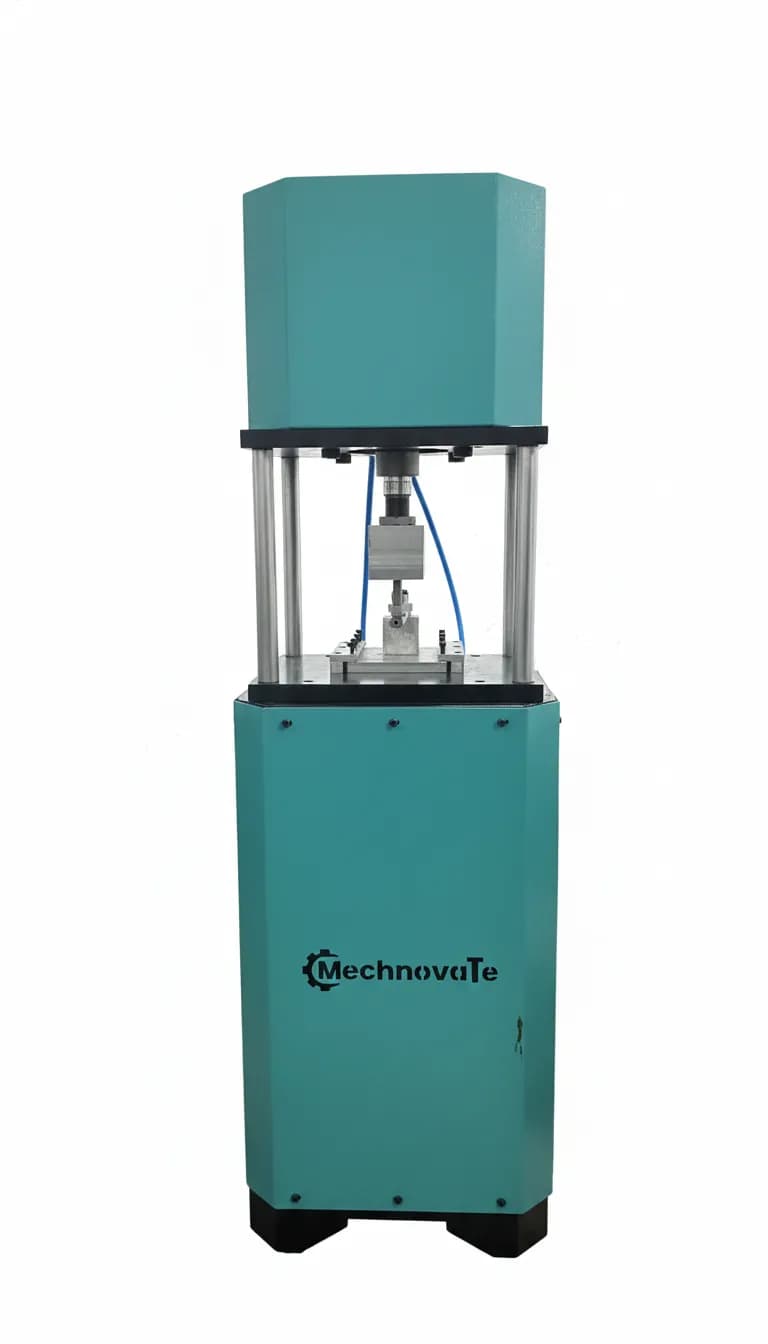
Select the Right Aluminium Punching Machine in Jaipur
Stop Profile Damage: The Engineering Solution for Jaipur Fabricators
If you are running a window fabrication unit in industrial areas like Vishwakarma (VKI) or Sitapura, you know that profile damage during the punching process is the single biggest contributor to material waste. High-quality sliding windows require clean, burr-free slots for locks, rollers, and water drainage. When an Aluminium Punching Machine is poorly calibrated or uses substandard dies, it causes 'drawing'—where the metal pulls inward—or 'cracking' around the hole edges. To eliminate this, you must prioritize machines with high-precision guide pillars and a pneumatic system capable of maintaining a consistent 6-8 bar pressure. For workshops transitioning from local assembly to professional manufacturing, selecting the right Manual Punching Machine or pneumatic variant is the difference between a 10% rejection rate and a 0.5% rejection rate.
Case Study: Reducing Rejection in a Jaipur Sitapura Workshop
Last year, we worked with a high-volume fabricator in Jaipur who was struggling with a 12% rejection rate on their premium anodized sections. The issue was twofold: inconsistent stroke speed and tool wear. We implemented a technical overhaul using the following steps:
- Baseline Audit: We measured the existing die clearance and found it was 0.25mm, which was far too wide for the 1.2mm profiles they were using.
- Equipment Upgrade: We replaced their local machines with a high-speed pneumatic unit and a Copy Router Machine for complex lock-hole geometries.
- Pressure Calibration: We installed a dedicated air reservoir to ensure that the pneumatic cylinder hit the profile with a consistent force of 15kN without pressure drops.
- Results: After six weeks, the waste was reduced to less than 2%, and the production speed increased from 45 frames to 75 frames per day. The ROI on the new equipment was achieved in just four months purely through material savings.
Technical Specifications That Prevent Profile Deformation
To ensure your aluminium profile cutting machine and punching units don't ruin your stock, you must look for specific engineering benchmarks. All Mechnovate machinery adheres to rigorous industrial standards like IS 1285 for aluminium alloys. Here are the specs you need to demand:
- Die Material: Look for HCHCr (High Carbon High Chromium) or D2 steel hardened to 58-60 HRC. This ensures the cutting edges stay sharp for over 100,000 cycles.
- Die Clearance: For a standard 1.5mm aluminium profile, your die clearance should be precisely 0.08mm to 0.12mm. Anything wider causes burrs; anything tighter causes excessive tool wear.
- Pneumatic Cylinder Bore: A minimum of 100mm to 125mm bore is required to generate the necessary force for multi-hole dies without stalling.
- Stroke Adjustment: The machine must have a mechanical stop to prevent the punch from over-traveling, which is a common cause of bottom-profile denting.
Common Mistakes in Jaipur Workshops: Why Your Profiles Are Cracking
Many fabricators in Rajasthan attempt to save costs by using a single die set for multiple profile thicknesses. This is a critical error. An aluminium cutter machine price might seem attractive, but if the machine lacks the rigidity to hold a profile firmly, the 'kickback' during the punch will bend the extrusion. Another mistake is neglecting the 'oil-mist' lubrication. In the dry, dusty climate of Jaipur, friction between the punch and the profile heat-welds small aluminium particles to the tool, leading to 'galling' and rough holes. Always ensure your upvc windows manufacturing machine or aluminium units are kept in a temperature-controlled or well-ventilated area to prevent thermal expansion of the jigs.
Comparison: Manual vs. Pneumatic Punching Systems
| Feature | Manual Punching Machine | Pneumatic Aluminium Punching Machine |
|---|---|---|
| Best For | Startups & Small Batches | High-Volume Production |
| Accuracy | Dependent on Operator Fatigue | 99.9% Repeatable Precision |
| Profile Safety | Moderate risk of scratching | High (with integrated clamps) |
| Maintenance | Low (Greasing only) | Moderate (Pneumatic seals & filters) |
| Speed | 2-3 slots per minute | 10-12 slots per minute |
For those scaling up, investing in an automatic upvc window plant cost India often includes these pneumatic stations as standard equipment. If you are looking for upvc machinery manufacturer options, remember that the same precision logic applies to upvc window manufacturing machinery.
Maintenance Protocols for Long-Term Precision
To keep your aluminium window fabrication machine running at peak performance in Jaipur’s environment, follow this engineering checklist:
- Daily: Clean the die bed of all swarf and chips. Aluminium chips are abrasive and will score your profiles if left in the machine.
- Weekly: Check the FRL (Filter, Regulator, Lubricator) unit. Drain the water trap to prevent moisture from rusting the internal valves of your upvc welding machine.
- Monthly: Inspect the guide pillars for play. If there is more than 0.05mm of lateral movement, your punch will eventually hit the die edge and shatter.
- Bi-Annually: Professional sharpening of the punch tips. A dull punch requires 30% more force, which increases the risk of profile deformation.
FAQ: Essential Questions for Fabricators
Q1: Can I use the same punching machine for uPVC and Aluminium? No. While some upvc window manufacturing machines look similar, the cutting angles and forces required for aluminium (a non-ferrous metal) are significantly higher than those for uPVC. Using an aluminium profile punching machine on uPVC might work, but using a uPVC machine on aluminium will likely destroy the motor or the pneumatic seals.
Q2: What is the ideal air pressure for a 5-ton punching machine? You should maintain a consistent 6 to 8 bar. If your workshop pressure drops below 5 bar, the punch will move slowly, causing the aluminium to 'tear' rather than 'shear,' resulting in a poor finish.
Q3: Why are my drainage holes off-center? This is usually due to poor clamping or a worn-out centering jig. Ensure your aluminium window corner crimping machine price includes high-quality pneumatic clamps that lock the profile against the back fence before the tool engages.
Get more articles like this
Follow Mechnovate on Google to see our guides in Google Discover & News